


How Surface Treatment Thickness Changes Snap Button Fit, Closing Force and Release Consistency
Why a Decorative Finish Becomes a Mechanical Dimension
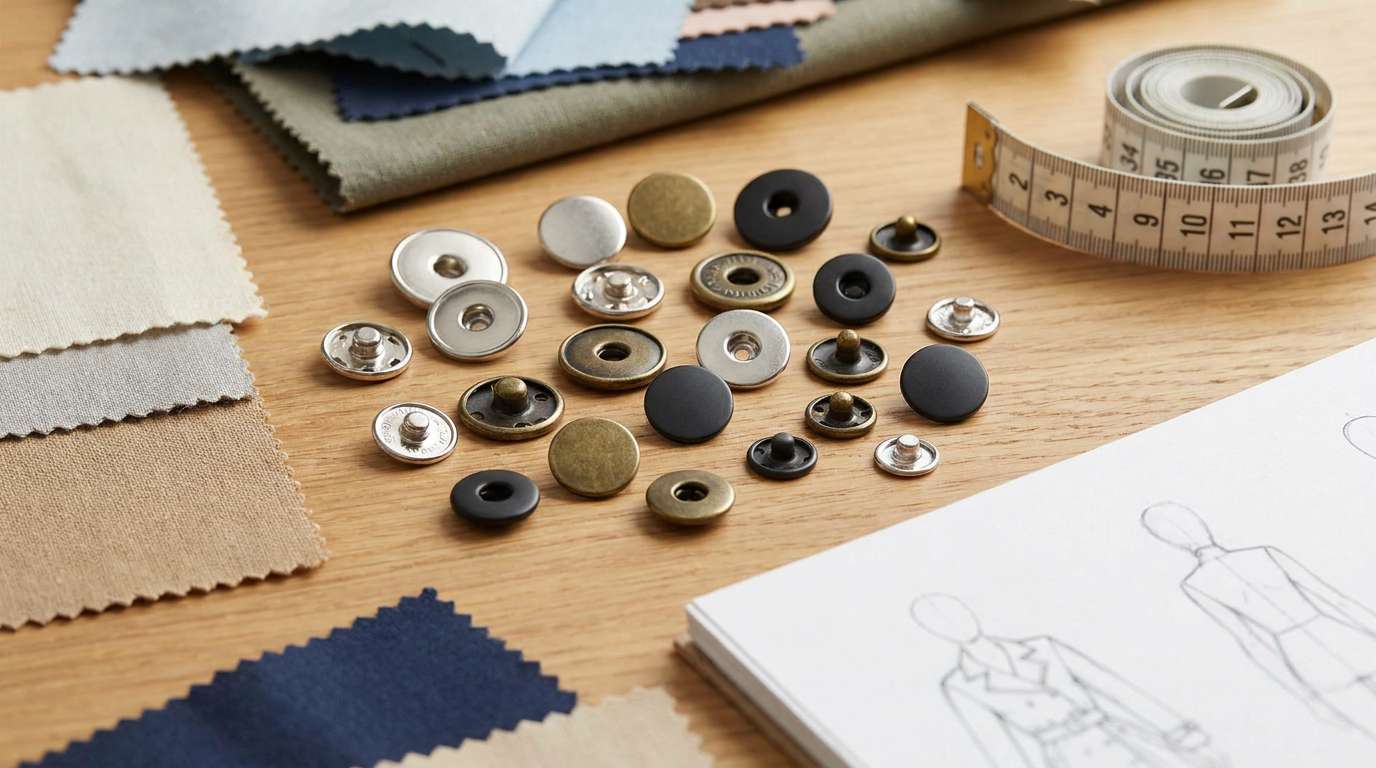
A snap button is a small assembly, but it operates through controlled interference. The stud enters the socket, the spring element deflects, the mating geometry passes a resistance peak, and the spring then settles into a retained position. Because the clearances are small, a surface treatment is not merely a color added after the mechanical design is complete. Its thickness becomes part of the finished dimensions.
This distinction matters whenever a buyer changes from nickel plating to black nickel, PVD, black oxide, paint, enamel, or powder coating. Two finishes can look similar while adding very different amounts of material to the functional surfaces. A design that closes smoothly in bare metal may become tight after coating. A design adjusted to accept a thick decorative layer may feel loose when produced with a thinner process. The correct specification therefore connects the base-metal drawing, the finished-part drawing, the coating process, and the required force window.
The practical purchasing question is not simply “Which finish looks best?” It is “Which finish system delivers the required appearance without moving the assembled snap outside its dimensional and force tolerances?”
The Clearance Stack Between Stud, Socket and Spring
For a male and female snap fastener pair, coating can affect both sides of the interface. A layer on the outside of the stud increases its effective diameter. A layer on the inside of the socket decreases the available opening. If both components receive the same uniform layer, the loss of diametral clearance is greater than the nominal thickness written on a coating certificate.
An idealized example makes this easier to visualize. If a layer of thickness t forms on every relevant surface, the stud diameter grows by approximately 2t, while the socket opening can shrink by approximately 2t. The theoretical diametral clearance can therefore change by about 4t. Real snap geometry is more complicated: recessed areas, edges, spring slots, contact bands and shielding can all receive different deposits. The example is not a production formula; it explains why a seemingly small coating change can create a noticeable force change.
The cap and post also belong to the dimensional stack. The snap fastener post length must still provide the correct material allowance after the snap is set through the fabric or leather. A thick coating on the post, rivet zone or mating barrel can change insertion, forming and rollover behavior. If the process reduces usable engagement or introduces brittle buildup in a forming zone, the setting result may vary even when the visible cap looks perfect.
Closing Force Is Controlled by Geometry and Friction Together
Closing force is the peak load needed to push the stud through the socket’s resisting feature. The spring must deflect, and the contact surfaces must slide against one another. Surface-treatment thickness changes the geometric interference, while the finish’s hardness, roughness and lubrication condition change friction. These effects act together.
A thicker deposit on the stud contact band usually increases interference if the socket geometry is unchanged. The spring deflects farther, contact pressure rises, and more force is required. However, thickness alone does not predict the result. A smooth, hard coating and a rough, high-friction coating of equal thickness can produce different force curves. Edge buildup can create a sharp initial resistance peak, while an evenly distributed deposit may create a smoother transition.
The same principle applies to different spring structures. An S spring snap button concentrates elastic movement in a particular socket geometry, so local deposit around the spring path can strongly influence entry and release. A parallel spring snap fastener distributes deflection differently, but its force is still sensitive to the finished stud profile, spring opening, surface friction and assembly alignment. Buyers should never transfer a coating specification from one snap structure to another without confirmation testing.
Release Force Does Not Always Change in the Same Direction
Release force is related to closing force, but it is not a mirror image. During opening, the stud must climb back across the retaining geometry while the spring unloads. The contact path, surface wear, edge shape and friction state may differ from those present during closing.
A thicker coating may increase both closing and release force, but several other outcomes are possible. A brittle layer can crack during the first closures and lower later forces. A soft coating can burnish, smear or transfer to the mating surface. A rough deposit may produce high initial force and then settle after a short wear-in period. If coating buildup rounds a retaining shoulder rather than enlarging the intended interference band, release resistance can even decrease while closing remains difficult.
For this reason, a specification should separate closing force, release force and retention under service loading. The phrase snap fastener resistance to unsnapping describes a functional requirement, not a substitute for the complete force profile. A reliable snap should close within the user’s ergonomic range, stay engaged during use, and release consistently when intentionally opened.
Consistency Depends on Thickness Distribution, Not Only Average Thickness
An average coating thickness can look acceptable while individual functional areas fall outside the useful range. Snap components include outer domes, recessed sockets, spring gaps, rolled edges, grooves and narrow contact bands. Each process reaches these features differently.
- Electroplating: Current density, part orientation, rack or barrel loading and shielding affect local buildup. Exposed edges may receive more deposit than deep recesses.
- PVD: The deposited layer is generally thin, but line-of-sight conditions, fixturing and rotation influence coverage. Substrate preparation and any underlayer still matter.
- Black oxide: This conversion treatment adds little dimensional build compared with paint or powder, but the material compatibility, sealing method and corrosion expectation must be defined.
- Liquid paint or enamel: Flow, curing, pooling and edge coverage create variation. Decorative cap areas are easier to control than small mating surfaces.
- Powder coating: The layer is comparatively high-build. Electrostatic attraction, Faraday-cage effects, cure flow and part orientation can make functional clearances unpredictable unless those areas are masked or designed for the process.
Lot consistency therefore depends on the thickness range at specified measurement points, not only a single average from a witness panel. The supplier should identify which surfaces control fit and measure or gauge those areas after finishing.
Why Thick Powder Coating Is Usually Kept Away From Mating Surfaces
Powder coating offers broad color options, durable coverage and efficient finishing for suitable parts. Its thickness is also the main reason it must be applied selectively on small snap components. A decorative cap shell has more tolerance for buildup than a stud neck, socket throat or spring contact path.
If powder reaches the engagement zone, it can reduce clearance, bridge slots, soften sharp functional geometry and create variable high spots. The first closure may shave or crush the film, leaving debris inside the socket. That damage changes later force measurements and can expose the substrate at precisely the surfaces receiving repeated wear.
A better approach is often to limit powder to the visible cap, mask functional surfaces, or engineer a separate decorative cap construction. The production route should be agreed before tooling is finalized, because masking access, hanging points, cure temperature and part handling affect cost and repeatability.
Plating and PVD Require Finished-Dimension Control
Electroplating and PVD are normally much thinner than powder coating, but they still affect snap behavior because the design clearance is small. A plated underlayer plus a decorative top layer must be considered as a system. It is not sufficient to control only the final-color layer if the total stack determines the finished dimension.
Plating can also change surface hardness and friction. If the mating parts use different coating stacks, the harder surface may polish or wear the softer one. PVD can provide a thin, hard decorative surface, yet its performance depends on adhesion, substrate smoothness, underlayers and the severity of repeated contact. Neither process eliminates the need for force testing on finished production parts.
The drawing should state whether the dimensional tolerance applies before or after finishing. For functional diameters and openings, after-finish dimensions are usually the more useful purchasing control. The process plan can then compensate the base geometry so the finished components meet the required fit.
Black Oxide Has Low Build but Is Not Dimensionally Invisible
Black oxide is attractive where a dark appearance and minimal dimensional change are priorities on a compatible ferrous substrate. It is a conversion process rather than a thick applied film, so it normally creates far less buildup than paint or powder.
“Low build” should not be interpreted as “no process effect.” Surface preparation can alter roughness, and sealing or oiling changes friction. Residual chemicals, inconsistent cleaning or variable post-treatment can affect tactile behavior and corrosion performance. The finished snap still requires closure and release checks, especially if the spring contact is sensitive or the product must operate without oily residue.
Paint and Enamel Work Best When Decoration Is Separated From Engagement
Liquid color systems are valuable for fashion hardware because they support custom shades, gloss levels and visual effects. Their behavior is less suitable for sliding contact bands. A painted functional surface may stick, chip or wear rapidly, while the same coating can perform well on a cap face that sees limited mechanical contact.
Designers should define the boundary between visible decoration and functional engagement. This allows the coating supplier to mask the socket interior, stud neck, post-forming zone or other critical surfaces. It also makes inspection clearer: color and appearance are judged on the visible area, while dimensions and force are judged on the mating system.
Common Symptoms of a Thickness Mismatch
The search question why snap buttons are hard to close often points to more than one possible cause. Excessive coating buildup is one, but spring strength, stud geometry, off-center setting, fabric compression and mixed component lots can produce similar symptoms. Troubleshooting should therefore compare bare components, finished components and installed assemblies rather than blaming the coating immediately.
A snap button not closing properly may show partial engagement, a tilted stud, an unusually sharp force peak or rebound after pressure is released. Inspect for coating on the stud shoulder, deposits inside the socket, debris from a damaged film, distorted spring elements and insufficient post forming.
When a customer reports that a snap button won't snap together, the supplier should verify component compatibility before adjusting the setting machine. Mixing different stud and socket variants can create the same failure as excessive coating. Part identification, lot traceability and go/no-go gauges help separate a process mismatch from an installation problem.
A complaint that the snap button stud too tight usually means the finished interference exceeds the intended window. Corrective action may involve reducing local finish buildup, changing masking, adjusting base dimensions, improving component alignment or selecting a different spring configuration. Simply applying more press force can damage the cap, fabric or socket without solving the root cause.
Measure the Coating Where It Changes Function
Coating thickness measurements are most useful when their locations correspond to the snap’s contact mechanics. A reading on the center of a decorative cap does not prove that the stud neck or socket throat is within tolerance. The control plan should identify critical points and use a method appropriate to the substrate and coating.
Practical controls can include:
- Before-and-after dimensional comparison on representative parts
- Finished stud diameter at the engagement band
- Finished socket opening or functional gauge result
- Visual checks for edge buildup, pooling, bridges and bare spots
- Coating-thickness readings at agreed accessible locations
- Closing-force and release-force measurements over a defined sample size
- Cycle testing to identify wear-in, chipping or force drift
- Installation testing on the actual fabric, leather or technical textile
No single measurement replaces the others. Thickness data explains the process, dimensional data confirms fit, and force data confirms function.
Specify a Force Window, Not Only a Nominal Target
A single “typical” closing-force result hides production variation. Buyers need a minimum and maximum acceptance window based on the end use. The lower boundary prevents loose engagement and unintended opening. The upper boundary protects usability, fabric integrity and installation quality.
Release force also needs a window. A garment snap intended for frequent one-handed operation has a different requirement from a heavy textile closure. The sample plan should capture multiple cavities, racks or barrels, coating batches and assembly shifts when those variables can affect the result.
Force results should be recorded by cycle number. Initial force, stabilized force and end-of-test force answer different questions. A coating that produces excellent first-cycle retention but large force loss after repeated opening is not equivalent to one that stays stable throughout the target service life.
Pre-Finish and Post-Finish Tooling Decisions
The supplier can compensate for predictable coating buildup in the base-metal tooling, but this requires a stable finish specification. If the customer alternates between thin PVD, plated finishes and thick color coatings on one uncompensated geometry, one version may fit while another falls outside the force range.
There are several engineering options:
- Use separate base dimensions for different coating families.
- Mask the functional contact surfaces and keep one mechanical geometry.
- Finish decorative components separately before final assembly.
- Use selective plating or controlled shielding where the process supports it.
- Define a total coating stack rather than naming only the visible topcoat.
- Approve finished golden samples for each finish code.
The best option depends on order volume, color range, tooling budget, process capability and the consequence of inconsistent force.
How Fabric and Installation Interact With Finished Snap Geometry
A snap button does not operate in isolation. Fabric thickness, reinforcement, compressibility and coating can change component alignment after setting. A post that is correct for one substrate may be too long or too short for another. Excessive setting force can distort a socket and make a well-controlled finish appear to be the cause of tight operation.
Testing should use the production substrate, reinforcement layers and installation equipment. The installer should confirm die alignment, setting height and component orientation. Finished snaps should then be conditioned and tested after any washing, curing or environmental process expected in the final product.
This system-level check is especially important for coated technical textiles, dense leather, multilayer workwear and soft knit structures. Each substrate transmits setting pressure differently.
A Practical Comparison of Finish Families
| Finish Family | Relative Dimensional Build | Main Fit Risk | Preferred Control Approach |
|---|---|---|---|
| Electroplating | Thin, but total multilayer stack matters | Edge buildup and uneven deposit in complex geometry | Specify total stack and after-finish functional dimensions |
| PVD | Generally very thin | Coverage variation, friction change and adhesion on contact areas | Control substrate preparation, fixturing and finished force |
| Black oxide | Very low build | Friction and sealing variation rather than major dimensional buildup | Control cleaning, sealing and functional feel |
| Liquid paint or enamel | Moderate and flow-dependent | Pooling, sticking, chipping and edge thickness | Decorate visible surfaces and mask engagement zones |
| Powder coating | High relative build | Loss of clearance, bridged features and first-cycle film damage | Restrict to suitable visible parts or design compensated geometry |
Quality Approval Should Include Both Appearance and Mechanics
A color approval card cannot approve snap function. Conversely, a force report does not approve color, gloss, surface defects or shade consistency. The supplier and buyer should use two connected acceptance tracks.
Appearance Approval
- Color standard and acceptable shade range
- Gloss or matte level
- Coverage, texture, edge quality and visible defects
- Approved viewing conditions and comparison sample
Mechanical Approval
- Finished functional dimensions and gauges
- Closing- and release-force windows
- Retention and pull-out performance on the real substrate
- Cycle performance and force drift
- Coating adhesion and wear at contact points
Production release should require both tracks to pass. This prevents a visually attractive lot from entering assembly with unacceptable fit.
Material Choice Can Reduce Dependence on a Protective Film
The substrate remains important even when a decorative surface is specified. Brass, zinc alloy, steel, 304 stainless steel and 316 stainless steel respond differently to forming, pretreatment, plating and corrosion exposure. A coating should be qualified with the actual base material rather than approved on a generic test coupon alone.
Baocheng also supplies customized finished snap buttons and related components made from JSW20 ultra-low magnetic permeability stainless steel. JSW20 is valuable where the finished formed component must maintain extremely low magnetic response while also providing resistance to chloride-containing environments. It can support projects in which needle-detection compatibility, corrosion performance and precise forming must be considered together.
Baocheng supplies finished products and customized components made from JSW20; it does not sell JSW20 raw sheet or coil. Finish selection is still based on the required color, contact conditions and environment. Without project-specific comparative testing, chloride-corrosion performance should not be ranked against 316 by assumption.
How Baocheng Develops a Finish-Compatible Snap Button
Baocheng can evaluate the snap as one complete system: cap, socket, spring, stud or post, base material, coating stack, substrate, setting method and required force. Available project options include custom dimensions, different snap structures, color matching, samples, tooling evaluation and OEM production.
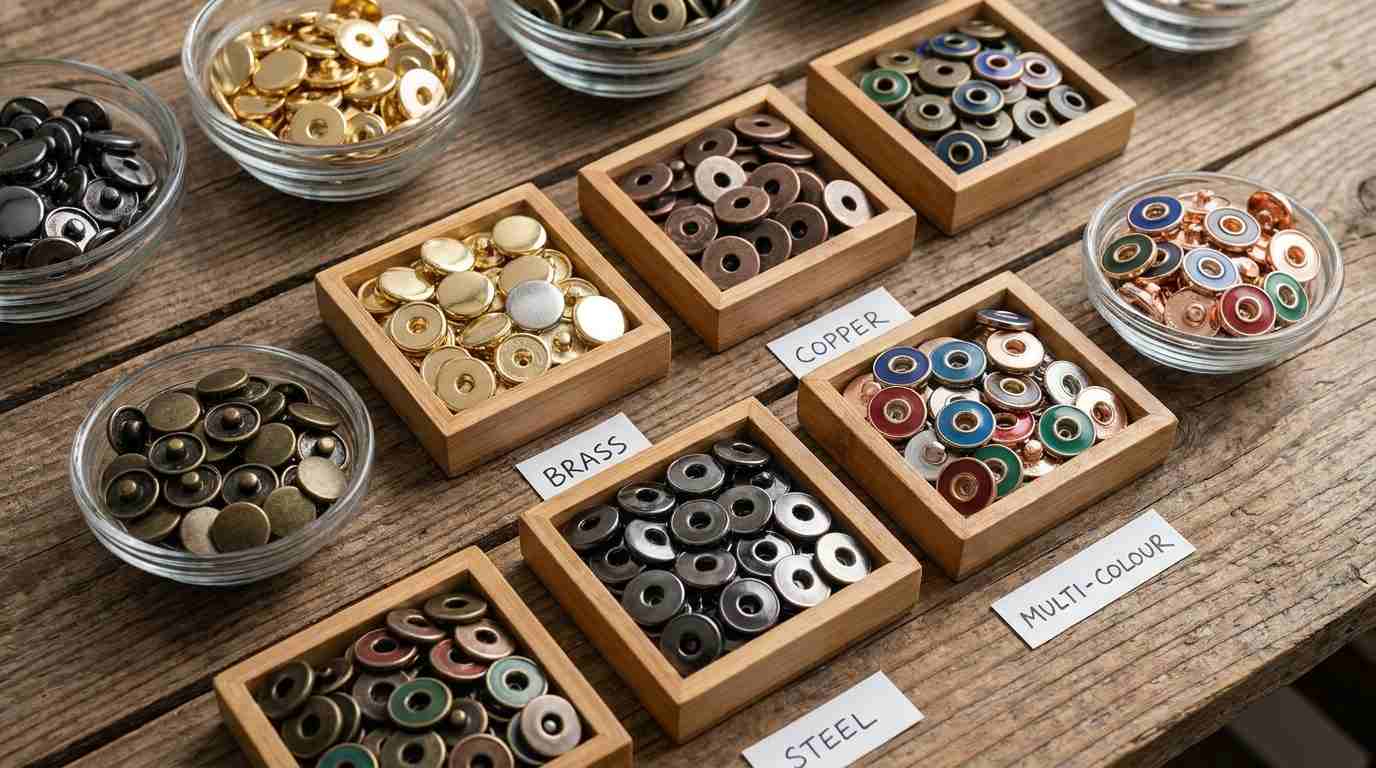
Material options can include brass, zinc alloy, steel, 304 stainless steel, 316 stainless steel and JSW20, depending on the structure and application. Surface options are selected around both appearance and functional clearance. For a new project, the most reliable route is to approve unfinished geometry first, confirm the proposed coating build, then validate finished samples on the actual substrate.
For repeat orders, the approved sample should be supported by measurable controls. Finish code, base material, component revision, coating stack, critical dimensions, force range and test condition should all appear in the controlled specification.
Buyer Checklist for Thickness-Sensitive Snap Buttons
- Define the exact snap structure and component combination.
- State the base material for every component.
- Name the complete finish system, including underlayers and topcoat.
- Identify which surfaces are decorative and which are functional.
- Specify masking or selective finishing where required.
- Apply critical dimensional tolerances to finished parts.
- Set acceptable closing- and release-force windows.
- Define cycle count and allowable force change.
- Test on the actual fabric, leather or industrial textile.
- Approve both appearance and mechanical golden samples.
- Maintain lot traceability for components and finish batches.
- Revalidate when the finish, supplier, substrate or geometry changes.
Final Decision: Design the Finish Into the Snap
Surface-treatment thickness changes the effective dimensions of the mating parts. That dimensional shift changes spring deflection, contact pressure, friction, closing force and release behavior. The average thickness value alone cannot guarantee consistency because local distribution, edge buildup, roughness, hardness and wear also matter.
The most reliable design treats coating as an engineering input from the beginning. Functional surfaces are identified, base geometry is compensated where necessary, decorative areas are separated from engagement zones, and finished assemblies are tested across a defined force window. This approach prevents late-stage adjustments on the setting line and produces a snap that looks correct, closes predictably and maintains its feel through service.
Focused FAQ
Can a few microns of plating noticeably change snap-button force?
Yes. Snap buttons operate with small clearances, and coating can build on both mating sides. The combined change in stud diameter and socket opening can noticeably alter interference and spring deflection.
Should snap dimensions be measured before or after finishing?
Base dimensions are useful for process control, but critical fit dimensions should also be specified and verified after finishing because the finished parts determine actual closing and release behavior.
Why can two lots with the same average coating thickness feel different?
Average thickness does not show local buildup at edges, contact bands or recessed areas. Differences in roughness, sealing, hardness and lubrication can also change friction even when average thickness is similar.
Is powder coating suitable for the socket and stud contact surfaces?
It is usually risky because powder is comparatively high-build and can reduce clearance or damage during first closure. It is generally better suited to selected visible surfaces unless the geometry is specifically designed and validated for it.
Does a higher closing force always mean better retention?
No. Excessive closing force can result from unwanted buildup, roughness or misalignment. Retention, intentional release, user ergonomics and durability must be evaluated separately.
Why does snap force change after several opening cycles?
Contact surfaces wear in. A coating may polish, compress, chip or transfer, changing friction and effective geometry. Recording force by cycle reveals whether the finished system stabilizes or continues to drift.
Can one base geometry be used for plating, PVD and powder coating?
Sometimes, if functional areas are masked and the finished dimensions remain controlled. High-build finishes often require separate compensation, selective application or a different component construction.
What information should a buyer send for a customized project?
Provide the snap structure, dimensions, base material, complete finish, color target, substrate layers, installation method, closing and release requirements, cycle target, environmental exposure and compliance needs.
Can Baocheng customize finished snap buttons for tight force tolerances?
Yes. Baocheng can evaluate structure, material, base geometry, finish distribution, installation and testing together, then provide samples and customized finished components for approval before mass production.
#SnapButtonCoating, #SurfaceTreatmentThickness, #SnapButtonFit, #ClosingForce, #ReleaseForce, #SnapFastenerEngineering, #PlatingThickness, #PVDCoating, #BlackOxide, #PowderCoating, #CustomSnapButtons, #JSW20, #BCNewMaterial