


Snap Button Cycle Testing: Measuring Force Drift, Wear and Service Life
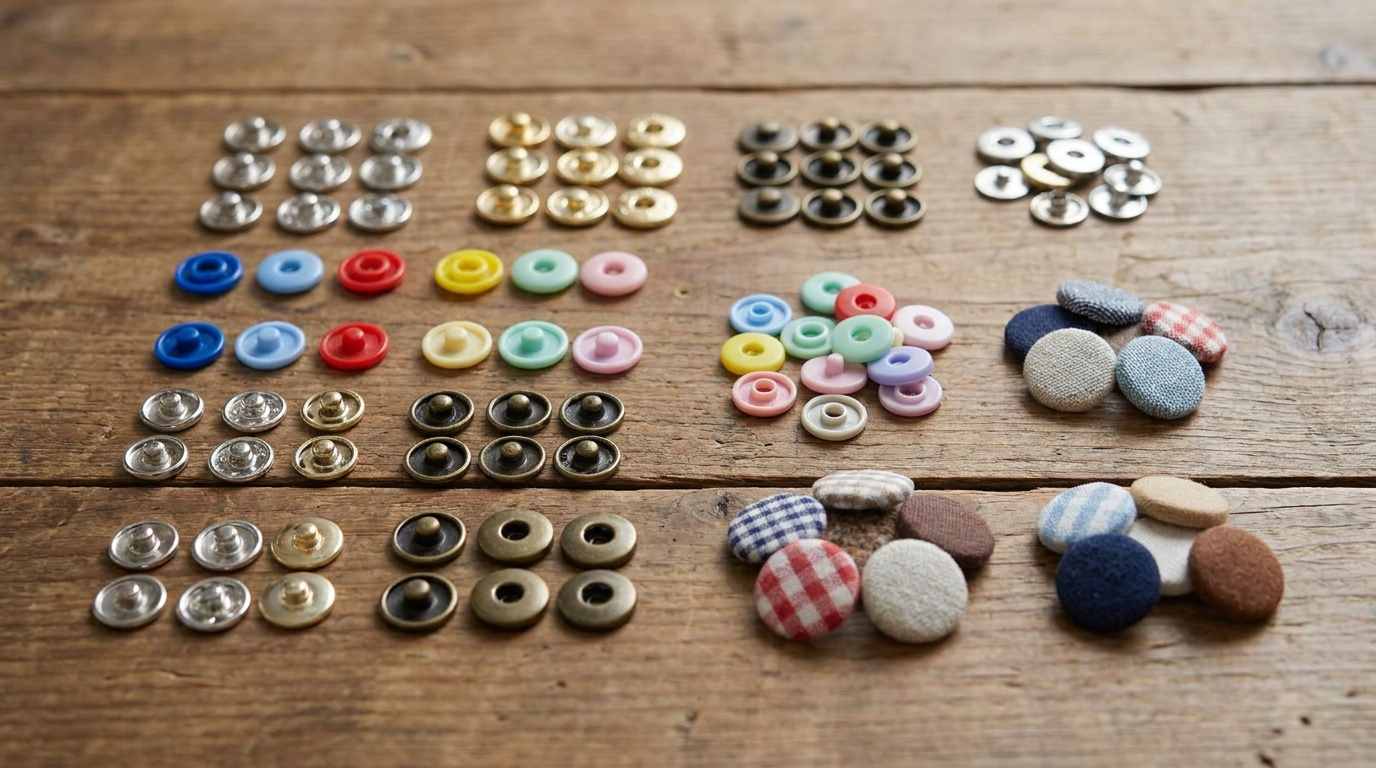
A new snap button can close with a clean click and release at an acceptable force, yet its performance may change rapidly after repeated use. Springs relax, contact surfaces polish, plating wears, posts loosen and the surrounding substrate flexes. These changes can reduce retention, increase operating force or create an unstable closure long before the rest of the product reaches its intended service life.
Cycle testing evaluates this time-dependent behavior by repeatedly closing and opening the same snap assembly under controlled conditions. The goal is not merely to count how many operations occur before complete breakage. A useful program measures force drift, observes wear and identifies the first point at which the closure no longer meets its functional or appearance requirements.
For sourcing and product-development teams, the central question is application-specific: how consistently must the snap perform over the expected life of the garment, bag, cover or technical textile? The answer determines specimen construction, cycle count, operating speed, measurement intervals, conditioning and acceptance criteria.
Define What One Cycle Means
One cycle should consist of one complete closing action followed by one complete opening action. The procedure must ensure full engagement during closing and full disengagement during opening. Partial engagement produces misleadingly low wear and may not load the spring or stud profile in the same way as normal use.
The test method should state whether the mechanism operates axially or through a controlled peel angle. It should also define travel, speed, dwell time and alignment. A machine that strikes the snap quickly may generate different wear from a slow tensile tester. Hand cycling can provide early development insight, but it introduces operator variation and is unsuitable as the only basis for production acceptance.
Cycle count is not a universal quality grade. A frequently opened garment closure, an occasional bag compartment and a seasonal cover have different duty patterns. The requirement should be derived from intended use, expected product life and consequences of failure.
Measure Baseline Performance Before Cycling
Every specimen should be characterized before the repeated operation begins. At minimum, record initial closing force, initial release force, installed alignment and visible condition. Where the application requires it, also record retention under a sustained load, cap rotation, attachment strength and dimensional checks.
Baseline measurements provide the reference for calculating change. Without them, a snap that ends the test at an acceptable force may be judged as stable even though it began unreasonably tight and lost most of its retention during cycling. Individual specimen histories are more informative than comparing only group averages at the start and finish.
Use fresh specimens for the baseline. Repeated hand checking before the formal test is already a form of conditioning and should be avoided or recorded. Identify each specimen so its force measurements, observations and failure mode remain connected throughout the program.
Build Specimens That Represent Production
Cycle behavior depends on the whole installed system. Components should come from production-intent tooling and finishes. They should be installed on the actual fabric, leather, coated textile or multilayer construction with the intended post or prongs, dies and machine settings.
Loose-component cycling is useful for isolating the socket-and-stud mechanism, but it cannot reveal substrate loosening, cap rotation, hole growth or attachment damage. Installed cycling shows how the closure interacts with the product. A robust validation program can use both, with each test answering a different question.
Specimen geometry should allow the fixture to operate the snap without artificially supporting the installed area. Reinforcement, seams, folds and coatings that exist in production should remain in the test piece. If several constructions use the same hardware, test the most demanding ones rather than assuming one result covers all locations.
Different Snap Structures Wear Differently
The spring or socket design controls how the stud is captured and released. Contact location, elastic deflection and friction determine the initial feel and the way force changes with use. A cycle requirement should therefore apply to an exact component combination, not a generic diameter.
A W style snap button can concentrate elastic action and contact in a different pattern from a ring-spring or parallel-spring design. Its acceptance window must be established from its own geometry, material and intended duty. Results should not be transferred between product families simply because the cap diameter looks similar.
open prong snap fasteners use prongs to penetrate and engage the substrate. During cycling, the mechanism may remain functional while the installed prongs begin to move, enlarge the holes or damage fibers. The inspection should therefore include the back of the attachment and surrounding fabric.
A closed cap prong snap may present a different external appearance while relying on similarly controlled prong formation. Cap support, prong alignment and substrate density affect whether the assembly stays flat and secure as the closure is operated repeatedly.
Structure comparisons are most useful when size, substrate and installation are controlled. Otherwise, an apparent durability difference may come from post length, fabric reinforcement or setting quality rather than the locking mechanism.
Use Measurement Intervals, Not Only an End Point
A snap can change quickly during early running-in, stabilize for a period and then deteriorate. Measuring only at the final cycle misses this pattern. Establish checkpoints appropriate to the target life, such as baseline, early cycles, intermediate stages and final evaluation.
At each checkpoint, record closing and release force using the same method. Avoid taking excessive measurements that add unplanned cycles or change the wear history. If specimens must be removed from an automatic fixture for testing, use a documented process that preserves alignment and identification.
Trend individual data and group statistics. Important indicators include:
- Percentage or absolute change from initial closing force;
- Percentage or absolute change from initial release force;
- Spread between the highest and lowest specimen;
- Number of specimens outside the approved window;
- Cycle at which the first functional or visual defect appears;
- Type and location of wear or deformation.
An average can remain acceptable while one specimen fails early. Acceptance rules should therefore include individual limits as well as group trends where the consequence of an unexpected opening is significant.
Closing-Force Drift and Release-Force Drift Tell Different Stories
A decline in release force may indicate spring relaxation, wear of the stud engagement surface, coating loss or permanent socket deformation. If the force becomes too low, the product may open unintentionally.
An increase in release force can result from galling, debris, corrosion products, distorted components or rough contact surfaces. The snap may remain closed securely but become difficult for the user to operate. A simultaneous increase in closing force suggests interference or alignment problems.
Closing force can decline while release force remains relatively stable if contact surfaces polish during running-in. This may be acceptable within a defined range. The decision should be based on user needs and closure security, not an assumption that every change is a failure.
Sudden jumps are different from gradual drift. A sharp change often points to a discrete event such as spring fracture, coating chip, component tilt or attachment movement. The specimen should be stopped and examined before additional cycles destroy the evidence.
Inspect Attachment Stability During the Test
The socket and stud can continue to mate even when the installed halves are loosening. Check cap rotation, vertical movement, post deformation, prong lift and substrate damage at each planned interval.
Marking the cap and fabric with aligned reference lines can help reveal rotation. A feeler check or controlled displacement measurement can detect lift. Photographs taken from consistent angles document gradual changes that are difficult to remember after the test.
If attachment movement begins, identify whether it comes from incomplete setting, unsuitable post length, excessive release force or substrate compression. Continuing to cycle until total separation may provide a failure count, but it should not replace analysis of the earlier onset.
Match the Cycle Program to the Application
The same snap family can experience very different service demands. Application-based testing translates an abstract cycle count into a credible use case.
Children’s Garments
metal snap buttons for baby clothes may be opened repeatedly during dressing and garment care. The validation should balance secure retention, manageable operating force, attachment integrity and surface condition. Testing must use the actual lightweight or multilayer babywear construction rather than a heavy laboratory fabric that masks substrate damage.
Jackets and Cuffs
snap buttons for jacket cuffs can experience frequent operation, off-axis pulling and local fabric bending. A straight axial cycle test may be supplemented with an opening motion that represents how the cuff is handled. Inspect the edge of the placket for progressive hole growth and cap tilt.
Stretch and Performance Apparel
snap buttons for activewear operate on substrates that may stretch, recover and carry perspiration. Cycle testing should control material tension and can include relevant conditioning. The snap should not become the rigid point that initiates tearing in an elastic construction.
Industrial Garments
heavy duty snaps for workwear are expected to tolerate repeated use, contamination and higher handling loads. A high initial release force is not enough. The system should maintain an acceptable operating window after cycling without sharp wear, attachment loosening or finish breakdown that interferes with function.
These examples show why one general cycle specification cannot cover every market. The approval should state the product location, user, substrate and service assumptions behind the selected requirement.
Combine Mechanical Cycling With Relevant Conditioning
Real products encounter more than dry mechanical operation. Washing, perspiration, humidity, salt, detergents, temperature changes and abrasive particles can alter contact surfaces and substrates. A risk-based program combines cycling with exposures relevant to the product.
Conditioning can occur before cycling, after cycling or in alternating stages. Pre-conditioning shows how an exposed snap begins its mechanical life. Post-conditioning reveals whether wear has damaged the protective finish. Alternating exposure and cycling can better represent repeated use and care, but the procedure must remain controlled and reproducible.
Do not combine every possible exposure into one test without a clear purpose. If a specimen fails, an overly complicated sequence makes the cause difficult to identify. Use baseline mechanical cycling first, then add targeted environmental conditions based on the expected service risk.
Surface Finish Influences Friction and Wear
Nickel plating, black nickel, antique finishes, paint, powder coating, PVD and other surface systems have different thickness, hardness and friction behavior. Functional contact areas may polish or wear through even when decorative surfaces remain attractive.
Inspect for scratches, flaking, transferred material, powdery debris, exposed substrate and color change. Coating fragments can raise operating force or interfere with spring movement. A finish change should trigger cycle revalidation because identical base geometry can behave differently after the contact surfaces change.
Film thickness also affects fit. Excess buildup on a stud or inside a socket can increase early force and accelerate wear. Uneven coverage can create specimen-to-specimen variation. Dimensional inspection after finishing should accompany the mechanical data.
Material and Forming Quality Affect Cycle Stability
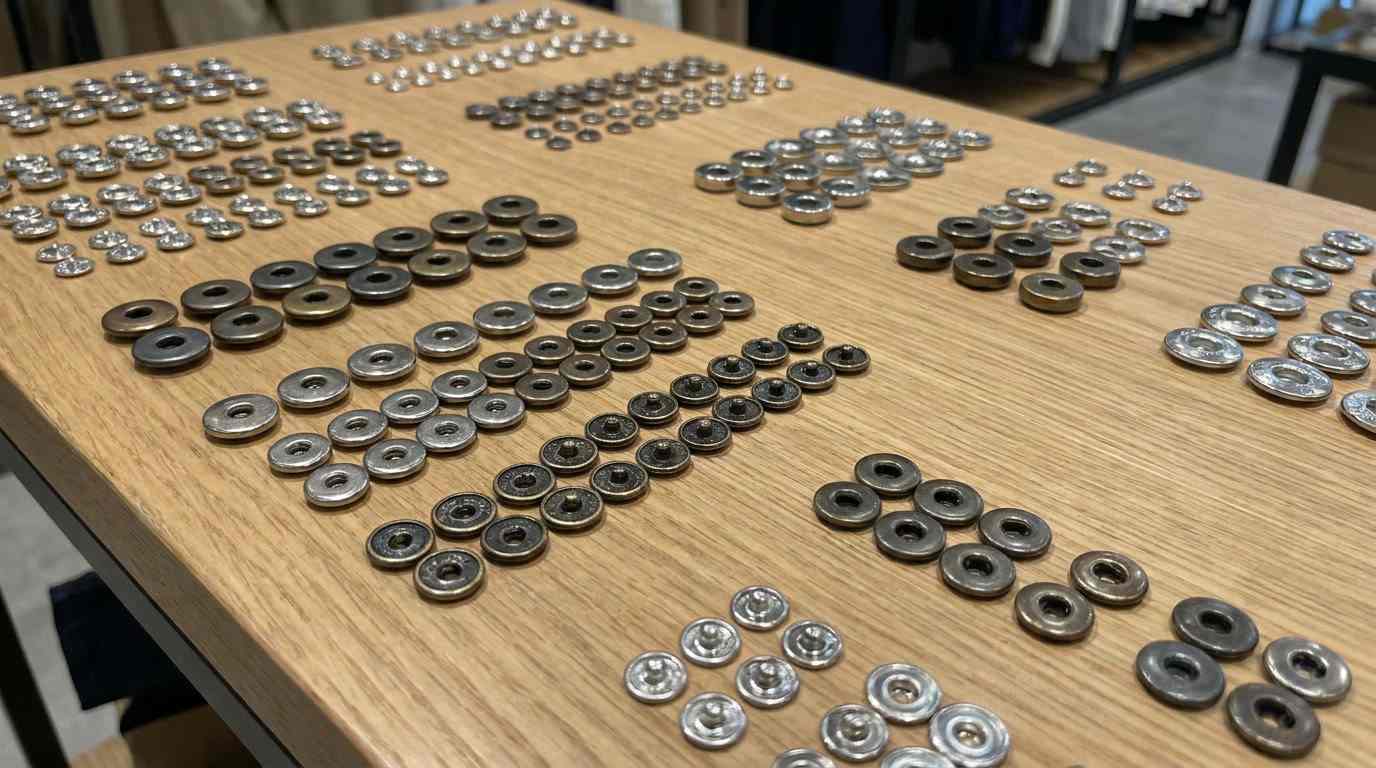
Spring response depends on material properties, forming history and geometry. Cracks, excessive work hardening, thinning, burrs and residual distortion can produce early failure. Posts and prongs must also retain attachment while the closure is repeatedly loaded.
Brass, steel, zinc alloy and stainless steel components should be evaluated as finished systems because material choice interacts with structure and surface treatment. A material with strong corrosion performance still needs suitable forming and spring behavior for the design.
For projects requiring very low magnetic response after forming, Baocheng can supply customized finished snap buttons and components made from JSW20 ultra-low magnetic permeability stainless steel. JSW20 combines extremely low magnetic permeability after deformation with resistance to chloride-containing environments. Cycle, force, corrosion and installed attachment performance should be verified on the final project design. Baocheng supplies finished products and customized components rather than JSW20 raw sheet or coil.
Baocheng can also develop finished snap systems in brass, zinc alloy, steel, 304 stainless steel and 316 stainless steel. Material, component structure, cap design, dimensions, finish, post length and substrate installation can be coordinated during sample development.
Control Fixture Alignment and Operating Speed
Misalignment can create artificial wear. The cycling fixture should bring the socket and stud together concentrically and apply the intended opening direction without bending the posts. It should accommodate the natural movement of the substrate without allowing uncontrolled twisting.
Operating speed influences impact, heat and dynamic force. Use a rate that reflects the test objective and remains repeatable. An accelerated test may run faster than normal service, but excessive speed can introduce failure modes that would not occur in use. Document dwell time if the snap remains closed under load between operations.
Fixtures also wear. Periodic alignment checks, maintenance and reference specimens help distinguish changes in the equipment from changes in the snap lot.
Define Failure Before the Test Starts
Complete fracture is only one failure. The protocol should identify all conditions that end or fail the test, including:
- Release force below the minimum security requirement;
- Closing or release force above the user-operability limit;
- Failure to achieve complete engagement;
- Unintended opening under a defined proof load;
- Spring cracking, permanent deformation or component fracture;
- Cap, post or prong loosening beyond the permitted limit;
- Substrate tearing or unacceptable hole growth;
- Finish damage beyond the approved appearance standard;
- Sharp edges, debris or other conditions that create a safety risk.
Define whether one failed specimen rejects the group or whether a sampling rule applies. The decision should reflect product risk and the purpose of the test.
Report the Data So It Supports Corrective Action
A strong report contains more than “passed 5,000 cycles.” It identifies the exact component set, material, finish, substrate, reinforcement, post or prongs, installation equipment, dies, machine settings, fixture, speed, cycle definition, conditioning and acceptance criteria.
Provide individual force values at each interval, visual observations, photographs and failure classifications. Plotting force against cycle count makes drift visible. Record the first defect cycle even if the specimen continues to operate.
When comparing lots or design variants, keep the method constant. If a fixture or speed changes, separate the data rather than treating it as one continuous historical trend.
Use Cycle Testing in Production Control
Full development testing does not need to be repeated on every carton, but production should include a surveillance plan. First-article checks confirm the approved component and installation combination. Periodic cycle testing can detect spring variation, finish changes, die wear or installation drift.
Trace results to component lots, finish batches, substrate rolls, machines and dates. If performance shifts, this information narrows the investigation. Retain approved reference samples and the test method revision so suppliers and buyers compare the same conditions.
Revalidation is appropriate when the socket or stud geometry changes, material changes, finish system changes, post or prong design changes, substrate construction changes or installation equipment changes. Even a visually minor modification can alter friction, elastic response or attachment stability.
A Practical Cycle-Test Checklist
- Define one complete closing-and-opening cycle.
- Use production-intent components and installed material stacks.
- Measure baseline closing and release force.
- Set checkpoints that reveal early, middle and late behavior.
- Control alignment, speed, travel and opening direction.
- Inspect spring condition, finish wear and attachment movement.
- Match cycle count and conditioning to the application.
- Use individual limits as well as group trends.
- Define functional, visual and attachment failures in advance.
- Document every change that requires revalidation.
Conclusion
Cycle testing turns an initial snap-button impression into evidence about long-term consistency. It shows how the spring, stud, finish, installed joint and substrate change through repeated opening and closing.
The most useful program records baseline force, measures at planned intervals, observes attachment and surface condition, matches the duty to the application and defines failure before testing begins. With controlled specimens, fixtures and reporting, cycle data helps buyers and manufacturers prevent gradual loosening, rising operating force, early wear and unexpected closure failure in mass-produced products.
Focused FAQ
How many cycles should a snap button survive?
There is no universal number for every product. The requirement should reflect expected use frequency, service life, substrate, user needs and consequences of failure. The same snap may need different validation for a fashion pocket and an industrial garment.
Should closing and release force be measured during cycling?
Yes. Measuring at defined intervals shows whether the snap is stable, running in, becoming loose or becoming difficult to operate. An end-point count alone can hide unacceptable force drift.
Can loose components be used for cycle testing?
They can isolate mechanism wear, but installed specimens are also necessary to evaluate post or prong stability, cap rotation and substrate damage. The two methods answer different questions.
Why does release force sometimes increase after cycling?
Possible causes include debris, galling, corrosion products, finish damage, distorted components or fixture misalignment. The specimen should be examined at the point of change rather than cycled until the original evidence is lost.
Should washing happen before or after cycle testing?
The sequence depends on the product risk. Testing before and after defined washing can separate mechanical wear from care-related change. Alternating washing and cycling may be appropriate when it represents actual service, provided the method is documented.
Can Baocheng develop snaps for a specified cycle requirement?
Yes. Baocheng can coordinate finished component structure, material, dimensions, finish, post or prong design, sampling and installation on the customer’s actual substrate. The cycle definition, force windows, conditioning and acceptance rules should be agreed before approval.
#SnapButtonCycleTesting, #SnapFastenerDurability, #RepeatedOpening, #ClosingForce, #ReleaseForce, #ForceDrift, #SpringWear, #AttachmentStability, #CustomSnapButtons, #JSW20, #BCNewMaterial